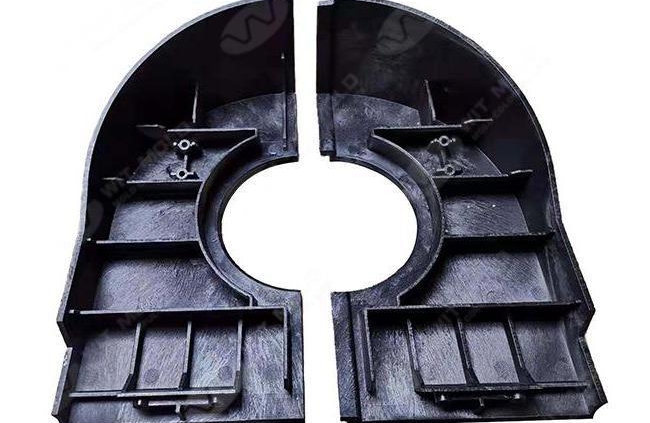
Advantages of Structural Foam Molds for Durable Plastic Parts

Durability is a critical requirement for large plastic components used in industrial machinery, material handling equipment, and commercial products. These parts must withstand mechanical loads, repeated handling, and long-term operating conditions without excessive deformation or premature damage.

Structural foam molding produces components with a cellular inner core surrounded by a relatively dense outer skin. This construction offers a practical combination of rigidity, reduced weight, and design flexibility.

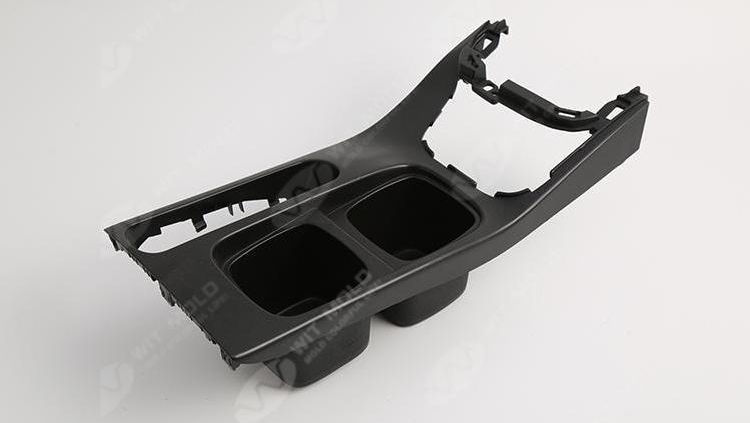
WIT Mold provides custom structural foam molding solutions for large plastic housings, panels, machine components, and industrial equipment enclosures.
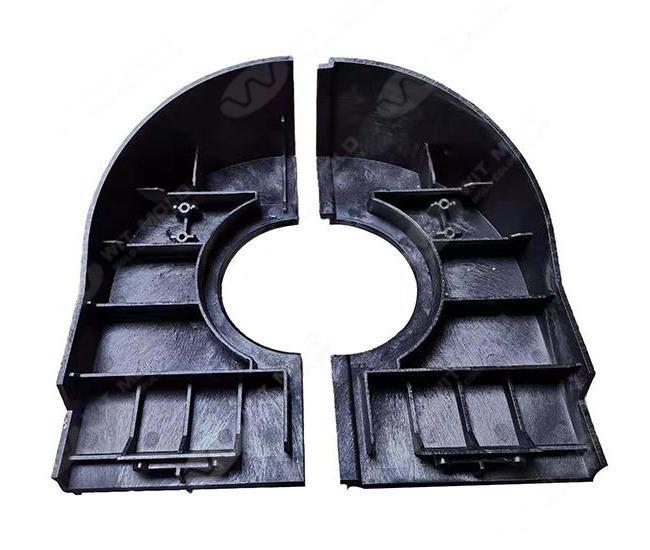
1. High Stiffness-to-Weight Ratio

One of the main advantages of structural foam molds is their ability to produce relatively rigid components without requiring completely solid plastic sections.

The cellular core reduces material density, while the outer skin contributes to bending resistance and structural stability.

This is particularly useful for:

  • Machine Housings: Large enclosures that require rigidity without excessive weight.
  • Industrial Panels: Wide components that must resist bending during handling and installation.
  • Equipment Chassis: Structural sections supporting internal components.
  • Material Handling Products: Large molded structures where weight and stiffness are important.

WIT Mold’s structural foam molding process supports components with a cellular core and solid outer layers, making it suitable for large structural plastic products.

2. Reduced Warpage and Internal Stress

Large injection molded components can develop warpage because of uneven shrinkage, cooling differences, and residual stress.

Low-pressure structural foam molding can help reduce some of these manufacturing problems.

Key advantages include:

  • Lower Cavity Pressure: Can reduce pressure-related stress during molding.
  • Improved Dimensional Stability: Suitable foamed structures may experience less distortion.
  • Thick-Section Molding: Supports substantial wall sections without requiring completely solid interiors.
  • Reduced Sink Marks: Controlled foaming can reduce visible shrinkage around thick features.

These benefits depend on material selection, component geometry, and processing conditions. Structural foam molding does not eliminate all dimensional defects.

3. Better Design Flexibility for Structural Components

Durable plastic products often require reinforcing ribs, mounting bosses, thick walls, and integrated supporting features.

Structural foam molding allows these elements to be incorporated into large molded components.

Structural FeatureDesign BenefitTypical Application
Thick WallsSupports rigid component constructionEquipment housings
Reinforcing RibsImproves stiffness in selected areasIndustrial panels
Mounting BossesIntegrates fastening featuresMachine enclosures
Large Structural SectionsSupports complex one-piece designsEquipment chassis
Cellular CoreReduces material densityPallets and bulk containers

Proper rib placement, wall thickness, and load distribution remain essential for achieving the required durability.

4. Impact Resistance for Industrial Applications

Structural foam molded parts can provide suitable impact performance when the correct resin, wall thickness, and component geometry are selected.

The dense outer skin contributes to surface integrity, while the cellular interior influences stiffness, energy absorption, and overall mechanical behavior.

Typical applications include:

  • Industrial protective covers exposed to routine handling.
  • Material handling containers subject to repeated movement.
  • Equipment housings requiring resistance to incidental impacts.
  • Commercial products with large structural surfaces.

However, structural foam is not automatically more impact-resistant than solid plastic. Actual performance must be verified using the specified material and appropriate impact testing.

5. Material Selection Influences Long-Term Durability

Different plastic materials provide different mechanical, thermal, and environmental properties.

WIT Mold supports structural foam molding projects using materials such as ABS, PC, PP, and other suitable engineering thermoplastics.

MaterialRelevant PropertyTypical Consideration
ABSImpact resistance and rigidityIndustrial housings
PCToughness and impact strengthProtective equipment components
PPChemical resistance and low densityContainers and material handling products
PPO/PPE-Based MaterialsDimensional stability and thermal propertiesIndustrial equipment parts
PBTRigidity and dimensional performanceSelected functional components

Material selection must consider operating temperature, chemical exposure, load conditions, and the specific resin grade.

6. Long-Term Performance Depends on Proper Mold Design

Durability is determined by more than material selection. Mold construction and processing conditions influence foam distribution, surface quality, and finished-part consistency.

Important engineering considerations include:

  • Wall Thickness: Maintain appropriate structural dimensions.
  • Foam Distribution: Control cellular development throughout suitable sections.
  • Gate Location: Support consistent filling of large components.
  • Cooling: Reduce uneven shrinkage and deformation.
  • Mounting Features: Provide sufficient strength around fastening points.
  • Surface Finish: Account for visible flow marks or secondary finishing requirements.

For projects requiring a completely solid structure or fine cosmetic details, conventional plastic molds may provide a more suitable manufacturing approach.

7. How to Verify Durability Before Production

Before approving a structural foam mold, OEM manufacturers should define the mechanical and dimensional requirements of the finished component.

Inspection or TestPurpose
Dimensional InspectionVerify critical assembly dimensions
Static Load TestingEvaluate deformation under specified loads
Impact TestingCheck resistance to expected impacts
Structural Stiffness TestingConfirm bending performance
Environmental TestingEvaluate behavior under relevant operating conditions
Sample InspectionCheck visible defects and molding consistency

The required tests depend on the product application. Load ratings, impact resistance, and expected service life should not be assumed without project-specific validation.

Frequently Asked Questions

Are structural foam molded parts durable enough for industrial equipment?

Yes, when properly designed and manufactured with suitable materials. Actual durability depends on component geometry, mechanical loads, operating conditions, and testing requirements.

Does structural foam molding reduce plastic part warpage?

It can reduce warpage in suitable thick-walled components through lower-pressure processing and controlled material distribution. Results depend on mold design and processing conditions.

Is structural foam molding suitable for load-bearing components?

It can be suitable for certain load-bearing applications, including pallets and equipment structures. Mechanical strength and long-term deformation must be verified for the intended loads.

Custom Structural Foam Mold Manufacturing With WIT Mold

WIT Mold manufactures custom structural foam molds for large plastic components requiring rigidity, dimensional stability, and dependable structural performance.

Our services cover mold engineering, tooling manufacturing, and production support for industrial housings, plastic panels, equipment components, and material handling products.

We develop tooling according to customer CAD drawings, resin specifications, load requirements, and expected production quantities.

Contact WIT Mold for Structural Foam Mold Manufacturing to discuss your project requirements and request a custom tooling quotation.
Applications That Require High Precision Injection Molding

High precision injection molding is essential for manufacturing plastic components that require tight dimensional tolerances, complex geometries, and consistent performance. Even small dimensional variations can affect assembly, mechanical movement, or product functionality in demanding applications.

WIT Mold provides precision injection molding and high-precision mold manufacturing solutions for automotive, medical, electronics, and industrial applications. With tooling experience since 2011, we manufacture precision molds according to customer drawings, material specifications, and production requirements.

1. Medical Devices and Healthcare Components

Medical equipment often contains small plastic components with detailed structures and strict dimensional requirements. Precision molding helps maintain consistent dimensions and reliable assembly.

Common applications include:

  • Diagnostic Equipment Components: Plastic housings and internal components requiring accurate alignment.
  • Medical Connectors: Small connection features with critical fitting dimensions.
  • Device Enclosures: Plastic parts that must accommodate electronic or mechanical assemblies.
  • Laboratory Equipment: Precision plastic components used in testing and measurement devices.

Medical applications may also require specific material, cleanliness, and regulatory controls, depending on the finished product. These requirements should be confirmed separately during project development.

2. Automotive Precision Components

Automotive systems rely on plastic components that must maintain dimensional consistency under repeated use and varying operating conditions.

Precision injection molding is particularly useful for:

  • Sensor Housings: Components requiring accurate positioning and stable assembly.
  • Electrical Connectors: Plastic bodies with precise contact spacing and retention features.
  • Automotive Lighting: Lens holders and optical component supports requiring accurate alignment.
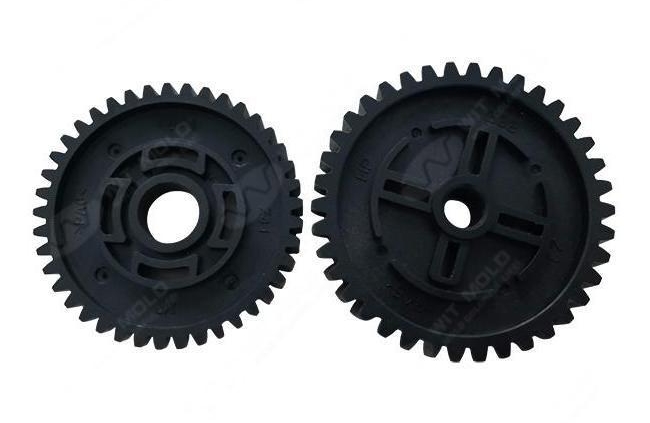
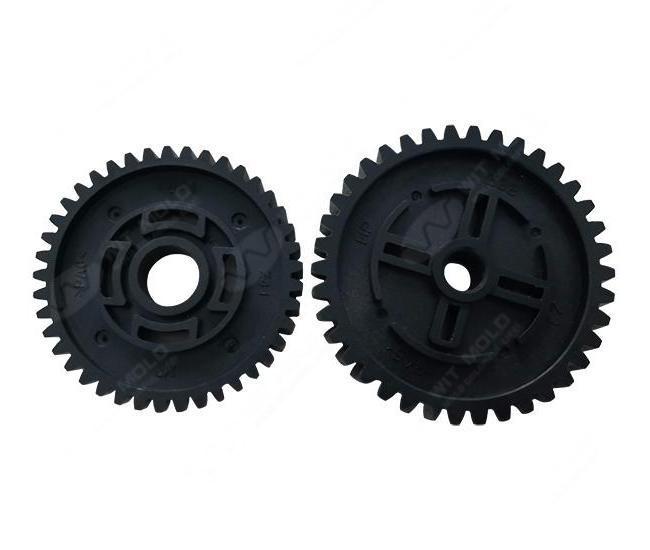
  • Mechanical Components: Small gears, clips, and functional parts with demanding dimensional requirements.

WIT Mold manufactures injection molds for automotive lighting, interior components, and other automotive applications. Mold design considers part geometry, material behavior, and critical assembly dimensions.

3. Electronics and Telecommunication Equipment

Electronic products frequently contain compact components with thin walls, small openings, and closely spaced assembly features.

Typical applications include:

  • Connector Housings: Require accurate pin positioning and cavity dimensions.
  • Switch Components: Need consistent movement and reliable mechanical fitting.
  • Communication Equipment: Precision plastic parts for connectors and internal assemblies.
  • Electronic Enclosures: Require dimensional accuracy for PCB mounting and component installation.

For products involving small, intricate features, high precision molds support detailed cavity construction and controlled dimensional requirements.

4. Optical and Instrument Components

Optical devices and precision instruments often require accurate positioning of lenses, sensors, and internal components.

Even minor dimensional deviations may affect optical alignment or measurement performance.

Common applications include:

  • Camera module frames and lens holders.
  • Optical sensor housings.
  • Instrument adjustment components.
  • Precision mounting structures.

Material selection, mold surface quality, and shrinkage control are important for maintaining the required dimensional and functional performance.

5. Precision Gears and Mechanical Parts

Small plastic gears, bearing supports, and sliding components require consistent geometry to operate correctly.

Precision molding is used when part dimensions directly influence movement, friction, or assembly accuracy.

ComponentCritical RequirementCommon Material Options
Plastic GearsTooth geometry and dimensional consistencyPOM, PA
Bearing HousingsAccurate bore dimensions and alignmentPOM, PA
Sliding ComponentsControlled dimensions and wear resistancePOM, PA
Mechanical ConnectorsConsistent fitting and retentionABS, PA, PC

Material suitability depends on the operating environment, loads, and specific resin grade.

When Is High Precision Injection Molding Necessary?

Not every plastic component requires precision tooling. The need depends on product functionality and acceptable dimensional variation.

Product RequirementWhy Precision Molding Matters
Tight Assembly TolerancesHelps components fit together correctly
Small or Intricate FeaturesSupports detailed cavity geometry
Moving Mechanical PartsMaintains accurate functional dimensions
Optical AlignmentSupports positioning of optical components
Multi-Part AssembliesReduces dimensional mismatch
High-Volume Precision PartsSupports consistent production quality

Precision injection molding requires coordinated control of mold machining, material shrinkage, processing conditions, and sample inspection.

Key Considerations Before Ordering Precision Injection Molds

Before starting a precision molding project, define the technical requirements that directly affect manufacturing accuracy.

  • Critical Tolerances: Identify dimensions that influence assembly or functionality.
  • Plastic Material: Specify the resin grade, shrinkage characteristics, and operating conditions.
  • Part Geometry: Evaluate thin walls, small features, and potential deformation risks.
  • Production Quantity: Determine suitable cavity configurations and tooling requirements.
  • Inspection Standards: Establish measurement methods and acceptance criteria.

WIT Mold incorporates engineering review, precision machining, mold trials, and sample verification into its tooling development process.

Frequently Asked Questions

What industries commonly use precision injection molding?

Precision injection molding is commonly used in medical devices, automotive systems, electronics, telecommunications, optical equipment, and industrial mechanical components.

What is the difference between standard and high precision injection molding?

Standard injection molding supports general dimensional requirements, while high precision injection molding requires tighter control over mold dimensions, material shrinkage, processing stability, and part inspection.

What affects the accuracy of precision molded parts?

Major factors include mold machining accuracy, material properties, cavity design, cooling conditions, injection molding parameters, and part geometry.

High Precision Injection Mold Manufacturing With WIT Mold

WIT Mold manufactures custom precision injection molds for applications requiring detailed geometries, reliable assembly, and dimensional consistency. Our precision mold manufacturing capabilities include complex mold components, precision gears, and structural plastic parts.

We develop tooling based on customer CAD drawings, critical tolerances, plastic material specifications, and production requirements.

Contact WIT Mold to request a precision injection mold quotation and discuss the technical requirements of your next project.

Guide to Choosing Plastic Molds Based on Product Requirements

Choosing the right plastic mold starts with understanding the finished product rather than selecting a mold structure first. Product function, material properties, dimensional tolerances, and production quantities all influence mold design and manufacturing costs.

WIT Mold has manufactured custom plastic molds since 2011, supplying injection tooling for automotive, household appliances, telecommunications, and industrial applications. Matching mold specifications to actual product requirements helps reduce unnecessary tooling expenses and manufacturing problems.

1. Define the Product’s Functional Requirements

The intended application determines many important mold design decisions. Components exposed to mechanical loads, high temperatures, or repeated assembly require different considerations from decorative plastic covers.

Product RequirementMold Design Consideration
Structural StrengthWall thickness, ribs, and material selection
Snap-Fit AssemblyUndercuts, draft angles, and ejection mechanisms
Threaded ConnectionsThread geometry and release mechanisms
Heat ResistanceMaterial compatibility and mold temperature control
Visible SurfacesGate positioning, parting lines, and surface finishing
Tight Assembly FitShrinkage allowances and dimensional control

For example, plastic enclosures with snap-fit features may require sliders or lifters, while components with complex threads may need specialized release mechanisms.

2. Select Mold Specifications Based on Plastic Materials

Different plastic resins have unique shrinkage rates, flow properties, and processing requirements. These characteristics affect cavity dimensions, cooling systems, and mold construction.

Plastic MaterialTypical Product ApplicationsMain Tooling Consideration
ABSAppliance housings, electronic enclosuresSurface quality and shrinkage
PPContainers, closures, functional componentsShrinkage and warpage control
PCProtective covers, transparent componentsProcessing temperature and surface quality
PA (Nylon)Gears, brackets, mechanical componentsDimensional changes and moisture sensitivity
POMPrecision gears and sliding partsShrinkage and dimensional consistency

WIT Mold works with various engineering plastics, including ABS, PC, PP, PA, POM, and other materials suitable for injection molding.

The specific resin grade and operating environment should be confirmed before finalizing the mold design.

3. Match Mold Accuracy to Product Tolerances

Not every plastic component requires the same dimensional accuracy.

General-purpose housings may allow wider dimensional variations, while precision mechanical components often require tighter control to maintain proper assembly and performance.

Important considerations include:

  • Critical Dimensions: Identify measurements that directly affect assembly or functionality.
  • Material Shrinkage: Account for dimensional changes during cooling.
  • Part Geometry: Thin walls and uneven sections can increase deformation risks.
  • Inspection Requirements: Establish measurement methods and acceptance criteria before tooling begins.

For demanding applications, WIT Mold manufactures high precision injection molds designed for components requiring accurate mold construction and dimensional consistency.

4. Consider Surface Appearance and Product Design

Surface finish requirements influence mold processing, polishing, texturing, and gate placement.

Different products may require smooth cosmetic surfaces, textured finishes, or specific visual characteristics.

  • Glossy Surfaces: Require suitable mold polishing and controlled molding conditions.
  • Textured Surfaces: Need appropriate surface treatment and sufficient draft angles.
  • Visible Plastic Housings: Benefit from careful gate and parting-line positioning.
  • Transparent Components: Require suitable materials, surface quality, and processing control.

Defining cosmetic requirements before mold construction helps avoid additional finishing work and design modifications.

5. Align Mold Design With Production Quantity

Expected production volume affects cavity count, tooling investment, and operating costs.

Production RequirementTooling ApproachMain Consideration
Lower Production QuantitiesSingle-cavity tooling where suitableManage initial investment
Medium Production QuantitiesSingle-cavity or multi-cavity toolingBalance cost and output
High Production QuantitiesMulti-cavity tooling where justifiedImprove production efficiency
Repeated Long-Term ProductionDurable mold constructionMaintain reliable operation

WIT Mold manufactures single-cavity and multi-cavity tooling, including high cavitation molds for applications requiring greater production output.

The final cavity configuration should account for part size, material flow, cooling requirements, and injection molding machine capacity.

6. Prepare Complete Product Specifications Before Ordering

Accurate technical information helps manufacturers recommend appropriate tooling and provide reliable quotations.

Before requesting a custom mold, prepare:

  • 3D CAD Files: Complete product geometry.
  • 2D Drawings: Critical dimensions and tolerances.
  • Material Specifications: Plastic type and required grade.
  • Production Volume: Estimated annual quantity.
  • Surface Requirements: Texture, finish, and appearance standards.
  • Functional Requirements: Assembly conditions, operating environment, and product performance.
  • Project Schedule: Expected tooling completion and production timeline.

WIT Mold’s manufacturing process includes engineering review, mold design approval, tooling construction, and sample verification before production.

Frequently Asked Questions

What is the most important factor when choosing a plastic mold?

Product geometry and functional requirements are fundamental because they determine the mold structure, material considerations, and necessary manufacturing processes.

Does plastic material affect mold design?

Yes. Different materials have different shrinkage characteristics, processing temperatures, and flow behavior, which influence cavity dimensions, runner systems, and cooling design.

How do I determine the right number of mold cavities?

Cavity count depends on production volume, part dimensions, material behavior, tooling budget, and molding machine capacity. Higher cavity counts can improve output but increase mold complexity and initial investment.

Custom Plastic Mold Manufacturing With WIT Mold

WIT Mold provides custom injection mold manufacturing based on product drawings, material specifications, dimensional requirements, and expected production quantities.

Our services include engineering review, mold design, manufacturing, and sample verification to support different OEM and industrial applications.

Contact WIT Mold for a Custom Mold Quotation to submit your CAD drawings and discuss the tooling requirements for your product.

Injection Mold Structures and Their Manufacturing Applications

Different plastic products require different injection mold structures to achieve accurate dimensions, reliable functionality, and efficient production. From simple plastic housings to complex automotive components, mold construction must accommodate product geometry, material behavior, and manufacturing requirements.

WIT Mold has specialized in custom plastic mold manufacturing since 2011, supplying injection molds for automotive, household appliance, telecommunications, and industrial applications. Understanding how mold structures relate to finished products helps OEM manufacturers develop suitable tooling solutions.

1. Conventional Mold Structures for Plastic Housings

Conventional injection molds are commonly used to manufacture plastic covers, enclosures, panels, and other components with relatively straightforward geometries.

These molds typically incorporate core and cavity plates, runner systems, cooling channels, and ejection mechanisms.

Typical manufacturing applications:

  • Electronic Enclosures: Plastic covers and housings requiring consistent dimensions and surface appearance.
  • Household Appliances: Control panels, external covers, and structural plastic components.
  • Industrial Equipment: Protective housings, mounting components, and machine covers.

Products containing side holes or undercuts may require additional sliders or lifters to enable proper part release.

2. Slider and Lifter Structures for Complex Components

Plastic parts with undercuts cannot always be removed through normal mold opening. Sliders and lifters provide controlled movement to release these features.

Sliders generally move sideways, while lifters combine angled movement with the ejection process.

Typical manufacturing applications:

  • Automotive interior panels with fastening features.
  • Electronic housings with side openings.
  • Plastic clips and snap-fit connectors.
  • Industrial components with internal or external undercuts.

The movement, clearance, and positioning of these mechanisms must be considered during mold design to prevent interference and premature wear.

3. Unscrewing Mold Structures for Threaded Products

Plastic components with certain internal or external threads require specialized release mechanisms.

Unscrewing molds use rotational movement to release threaded features before the molded part is ejected.

Common applications include:

  • Threaded plastic fittings and connectors.
  • Industrial caps and closures.
  • Components with precision thread profiles.
  • Plastic parts requiring reusable threaded connections.

This structure is particularly useful when the thread geometry cannot be released reliably through conventional stripping or mold-opening methods.

4. Multi-Cavity Mold Structures for High-Volume Production

Multi-cavity molds contain several identical cavities, allowing multiple plastic components to be manufactured during one injection cycle.

They are commonly used when production quantities justify increased tooling complexity.

Typical manufacturing applications:

  • Packaging components and closures.
  • Small consumer product components.
  • Electrical connectors and plastic fittings.
  • Repetitive industrial plastic parts.

WIT Mold manufactures single-cavity and multi-cavity tooling, with configurations of up to 32 cavities depending on product requirements. Our high cavitation molds are intended for applications requiring greater production output.

Balanced material distribution and effective cooling are important for maintaining cavity-to-cavity consistency.

5. Two-Shot Mold Structures for Multi-Material Components

Two-shot injection molds enable two different materials or colors to be molded into a single component through sequential injection stages.

This structure is commonly used when products require integrated functional or appearance features.

Typical manufacturing applications:

  • Automotive control buttons with multiple colors.
  • Plastic handles with soft-touch surfaces.
  • Electronic components combining rigid and flexible materials.
  • Consumer products requiring integrated grip features.

WIT Mold supplies two-shot injection molds for customized multi-material and multi-color plastic components.

Material compatibility, bonding performance, and mold alignment are important considerations for these projects.

6. Precision Mold Structures for Tight-Tolerance Components

Some products require tighter dimensional control than conventional plastic components.

Precision injection molds incorporate carefully manufactured cavities, inserts, and moving mechanisms to support demanding assembly and functional requirements.

Typical manufacturing applications:

  • Small mechanical components.
  • Electronic connectors and precision housings.
  • Automotive components with critical fitting dimensions.
  • Plastic parts requiring accurate alignment during assembly.

WIT Mold provides high precision injection molds for projects requiring detailed tooling construction and dimensional control.

Precision requirements can apply to conventional, multi-cavity, and specialized mold structures.

Injection Mold Structures and Application Comparison

Mold StructureTypical ProductsMain Manufacturing Requirement
Conventional MoldPlastic housings, covers, panelsDimensional consistency and surface quality
Slider/Lifter MoldClips, automotive panels, side-opening housingsReliable undercut release
Unscrewing MoldThreaded fittings and closuresAccurate thread formation and release
Multi-Cavity MoldPackaging parts, small plastic componentsHigh output and cavity consistency
Two-Shot MoldMulti-color buttons, soft-touch handlesMaterial compatibility and accurate alignment
Precision MoldElectronic and mechanical componentsTight dimensional control

How Product Requirements Influence Mold Structure

Several product characteristics determine the mold mechanisms required during manufacturing:

  • Geometry: Side holes, threads, and undercuts determine whether special release mechanisms are necessary.
  • Material: Shrinkage, processing temperature, and flow characteristics influence cavity and cooling design.
  • Production Quantity: Expected demand affects the number of cavities and tooling construction.
  • Dimensional Requirements: Critical tolerances influence machining, assembly, and inspection procedures.
  • Surface Appearance: Gate placement, parting lines, and surface finishing affect cosmetic quality.

A suitable mold structure should accommodate these requirements without introducing unnecessary mechanical complexity.

Frequently Asked Questions

Which mold structure is commonly used for automotive plastic parts?

Automotive components may use conventional molds, slider and lifter mechanisms, two-shot molds, or precision tooling depending on their geometry, materials, and functional requirements.

Why do some injection molds require sliders or lifters?

Sliders and lifters release undercuts that would otherwise prevent a molded component from being removed through normal mold opening and ejection.

Can multiple mold structures be combined?

Yes. A multi-cavity mold can incorporate sliders, lifters, hot runners, or other mechanisms when required by product design and manufacturing conditions.

Custom Injection Mold Manufacturing With WIT Mold

WIT Mold manufactures custom injection molds for different industrial applications, including conventional tooling, high-cavitation molds, precision molds, and specialized mold structures.

We provide mold design, manufacturing, and sample verification based on customer drawings, material specifications, and production requirements.

Contact WIT Mold to submit your product drawings and discuss suitable injection mold structures for your manufacturing project.

Comparison of Common Plastic Injection Mold Designs

Plastic injection mold designs directly influence manufacturing costs, production efficiency, and finished part quality. While different molds may produce similar plastic components, their structures, runner systems, and operating mechanisms can vary significantly.

WIT Mold has manufactured custom plastic molds since 2011, providing injection tooling for automotive, electronics, household appliances, and industrial applications. Understanding the differences between common mold designs helps product developers and OEM manufacturers make informed tooling decisions.

1. Two-Plate vs. Three-Plate Injection Molds

Two-plate and three-plate molds are among the most common structural designs used in plastic injection molding.

Two-Plate Injection Molds

A two-plate mold consists of a stationary side and a moving side, with one primary parting plane.

  • Advantages: Simple construction, relatively low tooling costs, and easier maintenance.
  • Limitations: Gate placement options may be more restricted, depending on the design.
  • Applications: Plastic housings, covers, containers, and general industrial components.

Three-Plate Injection Molds

A three-plate mold includes an additional separation plane, allowing the solidified runner to separate from molded parts during mold opening.

  • Advantages: Greater flexibility in gate positioning and automatic runner separation.
  • Limitations: More complex construction and generally higher tooling costs.
  • Applications: Multi-cavity components and products requiring specific gate locations.

Three-plate molds can be advantageous when direct gating near the center of a component is required.

2. Cold Runner vs. Hot Runner Mold Designs

The runner system controls how molten plastic travels from the injection molding machine into the mold cavities.

ComparisonCold Runner MoldHot Runner Mold
Initial Tooling CostGenerally lowerGenerally higher
Runner MaterialSolidifies and is ejectedRemains molten in heated channels
Material WasteGenerates solidified runnersCan reduce runner waste
MaintenanceRelatively simpleRequires additional temperature-control maintenance
Temperature ControlNo heated runner manifoldRequires controlled heating
Typical ApplicationsLow- to medium-volume production and varied projectsHigher-volume production where economics and material suitability justify it

Hot runner systems can reduce material waste and eliminate runner cooling requirements in suitable applications. However, they involve higher initial investment and additional maintenance considerations.

Cold runner systems remain a practical option for projects prioritizing simpler construction and lower tooling investment.

3. Single-Cavity vs. Multi-Cavity Mold Designs

The number of cavities determines how many plastic components can be produced during one injection molding cycle.

Single-Cavity Molds

Single-cavity designs produce one component per cycle. They are often suitable for larger products, smaller production quantities, or applications requiring simpler tooling.

Multi-Cavity Molds

Multi-cavity designs produce multiple identical components per cycle, increasing potential output.

WIT Mold manufactures single-cavity and multi-cavity tooling, with configurations of up to 32 cavities depending on project requirements. Our high cavitation molds support production applications requiring higher output.

Multi-cavity designs require careful consideration of runner balance, cooling performance, and cavity-to-cavity consistency.

4. Standard vs. Specialized Mold Mechanisms

Some plastic components cannot be produced efficiently using straightforward mold opening and ejection.

Specialized mechanisms accommodate complex product structures.

Mold DesignMain FeatureTypical Application
Standard Injection MoldConventional opening and ejectionHousings, covers, basic components
Slider MoldSide-action mechanism releases undercutsParts with side holes or external undercuts
Lifter MoldAngled movement releases internal undercutsClips and complex internal features
Unscrewing MoldRotational mechanism releases molded threadsThreaded caps and fittings
Two-Shot MoldSequential injection of two materials or colorsMulti-material handles and controls

Specialized molds generally require additional engineering and moving components, which can increase manufacturing costs and maintenance requirements.

5. Cost and Performance Comparison

Different mold designs involve trade-offs between initial investment, manufacturing complexity, and production efficiency.

Mold DesignRelative Tooling CostMain AdvantageMain Limitation
Two-PlateLowerSimple structureLess gate-placement flexibility
Three-PlateMediumFlexible gatingAdditional mold-opening complexity
Cold RunnerLowerSimple runner constructionSolidified runner material
Hot RunnerHigherReduced runner wasteHigher investment and maintenance
Single-CavityGenerally lowerSimpler cavity controlLimited output per cycle
Multi-CavityGenerally higherIncreased production outputMore complex balancing and cooling

These are general comparisons rather than fixed price rankings. Actual tooling costs depend on mold dimensions, steel selection, cavity count, part geometry, and other project specifications.

6. Factors That Influence Mold Design Decisions

Beyond the basic mold structure, several technical conditions affect tooling performance:

  • Part Geometry: Undercuts, threads, and complex surfaces may require additional mechanisms.
  • Plastic Material: Shrinkage, processing temperature, and resin characteristics influence runner and cooling design.
  • Production Quantity: Expected demand determines whether higher initial tooling investment is justified.
  • Gate Requirements: Cosmetic surfaces, weld lines, and filling behavior influence gate positioning.
  • Dimensional Accuracy: Critical tolerances require appropriate machining, cooling, and inspection controls.

The final mold structure should be evaluated through engineering design review before manufacturing begins.

Frequently Asked Questions

Is a three-plate mold better than a two-plate mold?

Not necessarily. Three-plate molds offer greater flexibility in gate placement and runner separation, while two-plate molds generally provide simpler construction and lower tooling costs.

Are hot runner molds always more economical?

No. Hot runner systems can reduce runner waste, but their higher initial cost and maintenance requirements may not be justified for every production volume or material.

Can different mold structures be combined?

Yes. A multi-cavity mold may use a hot runner system, while a conventional mold can incorporate sliders, lifters, or other specialized mechanisms. Mold features are selected according to product requirements.

Custom Plastic Injection Mold Design With WIT Mold

WIT Mold provides custom injection mold design and manufacturing for different product geometries, materials, and production requirements. Our tooling capabilities include conventional plastic molds, multi-cavity molds, precision tooling, and specialized mold structures.

We develop injection molds according to customer CAD drawings, technical specifications, and expected production quantities, with engineering review and sample verification integrated into the manufacturing process.

Contact WIT Mold for a Custom Injection Mold Quotation to discuss your mold structure, material requirements, and production needs.

How Collapse Core Molds Create Internal Undercuts

Internal undercuts allow plastic components to incorporate retaining grooves, locking features, and other functional details inside a molded opening. However, these features also prevent a conventional rigid core from being withdrawn directly after injection molding.

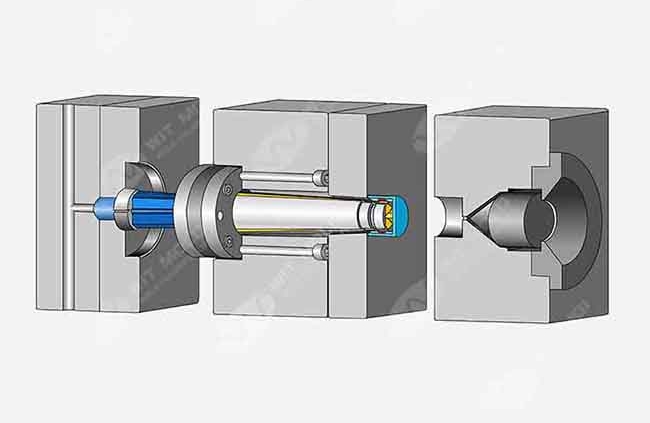
Collapse core molds solve this problem using a segmented core that moves inward before the finished component is ejected. This allows certain complex internal geometries to be molded without damaging the part during release.

WIT Mold manufactures custom injection tooling in China, including collapse core molds for specialized plastic part designs. We evaluate undercut geometry, material requirements, and core movement to develop suitable tooling structures for OEM projects.

1. Why Internal Undercuts Require Special Mold Mechanisms

An internal undercut is a feature that prevents a molded component from sliding directly off its forming core.

Common examples include internal retaining rings, circumferential grooves, locking shoulders, and selected threaded features.

With a fixed core, the undercut can mechanically trap the plastic component. Attempting to eject it without sufficient clearance may cause cracking, distortion, or damage to the molded feature.

A collapsible core provides clearance by reducing its effective diameter before ejection.

2. How the Collapse Core Mechanism Works

A typical collapsible core consists of movable segments supported by a central actuating mechanism. The segments remain expanded during injection to form the internal geometry.

After the plastic solidifies, the mechanism allows the segments to retract inward.

Molding StageCore MovementPurpose
Mold ClosingSegments move into molding positionForm the internal cavity and undercut
Plastic InjectionCore remains expandedMaintain the required internal geometry
CoolingCore supports the molded featuresAllow sufficient solidification
Core RetractionSegments collapse inwardClear internal undercuts
Part EjectionCollapsed core provides release clearanceRemove the component

The exact movement sequence depends on the collapsible core design and mold actuation system.

3. How Segmented Cores Form Internal Grooves

Consider a plastic component containing an internal circumferential retaining groove.

During injection, the expanded core has a corresponding raised feature that forms the groove inside the plastic part.

Once cooling is complete, the core cannot simply move out because the raised feature is locked behind the molded groove.

The collapsible core mechanism retracts its segments toward the center, reducing the effective core diameter until the groove is cleared.

Three dimensions are especially important:

  • Undercut Depth: Determines the radial clearance needed for release.
  • Internal Diameter: Limits the space available for core collapse.
  • Release Stroke: Must provide enough movement to avoid interference during ejection.

If the required radial movement exceeds the mechanism’s available collapse distance, a different mold structure or part redesign may be necessary.

4. Internal Undercut Design Requirements

Not every internal undercut can be produced using collapsible core tooling.

We evaluate the actual geometry before finalizing the mold design.

Design FactorEngineering Requirement
Undercut DepthMust remain within available collapse travel
Feature LocationMust allow clearance throughout retraction
Internal OpeningMust accommodate the collapsed core
Part Wall ThicknessMust support molding and ejection loads
Plastic MaterialShrinkage and rigidity affect release
Dimensional TolerancesCritical features require suitable core accuracy
Core Segment JointsWitness lines must be acceptable on functional surfaces

Parts with very small internal openings, deep undercuts, or complicated internal profiles may require alternative tooling.

For threaded components requiring rotational release, WIT Mold also supplies unscrewing molds.

5. Preventing Damage During Core Collapse and Ejection

A collapse core mold must release the internal features without transferring excessive force to the finished plastic component.

Common engineering concerns include:

  • Premature Retraction: Moving the core before sufficient cooling can deform internal features.
  • Insufficient Clearance: Incomplete collapse may damage the undercut during ejection.
  • Segment Misalignment: Poor alignment can affect dimensions and surface consistency.
  • Uneven Ejection: Unbalanced forces may distort or crack the molded component.
  • Core Wear: Repeated segment movement requires suitable fitting, lubrication, and maintenance.

WIT Mold’s design and engineering services include DFM analysis, mold flow analysis, and structural design review to support complex injection mold development.

6. Verifying Internal Undercuts During Mold Trials

Before tooling approval, the molded part should be checked for both dimensional accuracy and reliable release.

Inspection ItemAcceptance Focus
Undercut DimensionsDepth, profile, and position
Internal DiameterFit with mating components
Segment Witness LinesAcceptability on functional surfaces
Ejection QualityNo cracking or deformation
Mechanism OperationComplete and repeatable core movement
Assembly PerformanceProper engagement of locking or retaining features

Inspection requirements should follow the customer’s approved drawings and functional specifications.

WIT Mold’s quality system includes mold assembly inspections, mold trials, and manufacturing quality controls.

Frequently Asked Questions

How do collapse core molds release internal undercuts?

The core segments retract inward after molding, creating enough clearance to release the internal undercut before the part is ejected.

Can a collapsible core form internal threads?

Certain thread geometries are suitable, provided the core can collapse far enough to clear the thread profile. Other thread designs require an unscrewing mechanism.

What limits the maximum internal undercut depth?

The available radial collapse distance, internal opening, segment geometry, and required release clearance determine the practical limit.

Custom Collapse Core Mold Manufacturing With WIT Mold

WIT Mold manufactures custom injection molds for plastic components with internal undercuts, grooves, and complex release requirements.

We support mold engineering, precision machining, tooling assembly, and trial evaluation based on customer drawings and production specifications.

Contact WIT Mold to submit your 3D CAD models, internal undercut dimensions, resin specifications, and estimated production quantities for a custom collapse core mold quotation.

How to Select the Right Injection Mold Type for Your Product

Selecting the right injection mold type is essential for achieving consistent product quality, efficient production, and reasonable tooling costs. The best mold structure depends on your product geometry, plastic material, production volume, and dimensional requirements.

With injection mold manufacturing experience since 2011, WIT Mold provides custom plastic molds designed around different production requirements. The following selection process helps OEM companies and product developers determine suitable tooling configurations before manufacturing begins.

1. Start With Your Product Design

Product geometry is often the first factor determining injection mold structure. Simple components may use conventional molds, while complex features require additional mechanisms.

Product FeaturesRecommended Mold Solution
Simple housings and coversConventional two-plate mold
Internal or external threads requiring rotational releaseUnscrewing mold
Side holes and undercutsMold with sliders or lifters
Two materials or colorsTwo-shot injection mold
Metal inserts or embedded componentsInsert injection mold
Tight dimensional tolerancesPrecision-engineered injection mold

For example, plastic components with threaded features may require unscrewing molds, while products combining two materials can benefit from two-shot injection molds.

The proposed structure should be confirmed through a Design for Manufacturability (DFM) review before tooling production.

2. Determine Your Production Volume

Production quantity influences cavity count, mold construction, and long-term manufacturing costs.

  • Low-Volume Production: Single-cavity molds often provide a practical balance between initial tooling investment and production requirements.
  • Medium-Volume Production: Single-cavity or multi-cavity designs can be selected according to part dimensions, cycle time, and demand.
  • High-Volume Production: Multi-cavity molds can increase output per cycle and reduce unit costs when production quantities justify the investment.

WIT Mold supplies single-cavity and multi-cavity injection molds, with configurations of up to 32 cavities depending on project requirements.

For large production quantities, high cavitation molds can help increase manufacturing output while maintaining consistent part dimensions.

3. Consider Plastic Material Properties

Plastic material selection directly affects mold design, processing conditions, and dimensional stability.

Different resins have specific shrinkage characteristics, melt temperatures, and cooling requirements.

Plastic MaterialMain CharacteristicsMold Design Considerations
ABSImpact resistance and good surface finishShrinkage control and appearance
PPLightweight and chemical resistanceShrinkage and potential warpage
PCImpact strength and dimensional performanceProcessing temperature and cooling
PA (Nylon)Mechanical strength and wear resistanceMoisture sensitivity and dimensional changes
POMLow friction and good dimensional stabilityTemperature control and material-specific processing

The selected mold should accommodate the specified resin grade, rather than relying on general material properties alone.

WIT Mold supports injection molding projects involving ABS, PC, PP, PA, POM, and other engineering plastics.

4. Balance Tooling Cost and Production Efficiency

The lowest initial mold cost does not always result in the lowest total manufacturing cost.

Several tooling decisions influence long-term production economics:

  • Mold Steel: Material selection should reflect expected production life and processing conditions.
  • Cavity Count: More cavities increase potential output but also increase tooling complexity.
  • Runner System: Hot runners can reduce runner waste in suitable applications, while cold runners generally involve simpler tooling.
  • Cooling Efficiency: Appropriate cooling design can improve dimensional consistency and production cycle time.
  • Maintenance Requirements: Complex mechanisms may require additional inspection and maintenance.

For long-term production, the cost per acceptable part is often a more useful comparison than tooling price alone.

5. Confirm Dimensional and Surface Requirements

Products requiring tight tolerances, precise assembly, or specific surface finishes need additional attention during mold design.

Important factors include dimensional accuracy, cavity consistency, parting line placement, gate marks, and surface finishing.

For demanding components, suitable machining processes, material shrinkage allowances, and dimensional inspection procedures are necessary.

WIT Mold manufactures high precision injection molds for components with more demanding tooling and dimensional requirements.

Injection Mold Selection Checklist

Before finalizing your tooling requirements, prepare the following information:

Project RequirementInformation Needed
Product Design3D CAD files and 2D drawings
Plastic MaterialResin type and specific grade
Production VolumeEstimated annual quantity
Dimensional AccuracyCritical tolerances
Surface FinishAppearance, polishing, or texture
Product StructureThreads, undercuts, inserts, or multiple materials
BudgetTooling investment and target unit cost

These details allow manufacturers to evaluate suitable mold structures and prepare more accurate quotations.

Frequently Asked Questions

Which injection mold type is most suitable for high-volume production?

Multi-cavity molds are often suitable for high-volume production because multiple identical parts can be produced per cycle. However, the appropriate cavity count depends on product dimensions, material, and injection molding machine capacity.

Should I choose a hot runner or cold runner mold?

Cold runner molds generally have lower initial complexity, while hot runner systems can reduce runner waste and offer advantages in suitable high-volume applications. The choice depends on material compatibility, production quantity, and cost requirements.

Can injection mold types be changed after tooling production begins?

Some tooling modifications are possible, but major changes to cavity count, runner systems, or mold structure may require extensive rework or a new mold. Confirming the appropriate configuration during the design stage reduces this risk.

Custom Injection Mold Solutions From WIT Mold

WIT Mold manufactures custom injection molds based on customer drawings, material specifications, dimensional requirements, and production quantities. Our tooling capabilities cover conventional molds, precision molds, multi-cavity tooling, and specialized mold structures.

We provide engineering review, mold design, manufacturing, and sample verification to help customers develop tooling suitable for their production projects.

Contact WIT Mold to submit your CAD drawings and receive a custom injection mold quotation.

Structural Foam Molding vs Traditional Injection Molding

Structural foam molding and traditional injection molding are both used to manufacture thermoplastic components, but they differ in internal structure, molding pressure, tooling requirements, and finished-part appearance.

For large plastic housings, industrial panels, and structural components, choosing the appropriate process affects material consumption, production costs, and product performance.

WIT Mold provides structural foam molding and conventional injection mold manufacturing for OEM projects. Understanding their differences helps manufacturers select suitable tooling for large and complex plastic components.

1. Key Differences Between Structural Foam and Traditional Injection Molding

Traditional injection molding injects molten plastic into a mold cavity to produce a generally solid component. Structural foam molding introduces gas or a blowing agent into the plastic, creating a cellular core surrounded by a relatively dense outer skin.

Comparison FactorStructural Foam MoldingTraditional Injection Molding
Internal StructureCellular core with dense outer skinGenerally solid plastic
Molding PressureTypically lower in low-pressure structural foam processesGenerally higher
Part SizeParticularly suitable for large componentsSuitable for small to large components
Wall ThicknessFavors relatively thick sectionsSupports a wider range, including thin walls
Part WeightLower density in foamed regionsSolid material density
Surface FinishMay show swirl marks or surface irregularitiesOften better cosmetic finish
Tooling CostPotentially lower for large low-pressure moldsDepends on pressure and tooling requirements
Cycle TimeMay be longer for thick componentsDepends on part geometry and cooling

Neither process is universally better. The appropriate method depends on component specifications and manufacturing priorities.

2. Structural Performance and Material Distribution

Structural foam molding produces components with a cellular interior and relatively solid outer layers.

This construction can provide a useful stiffness-to-weight ratio for large products, including equipment housings and structural panels.

Structural foam molding is particularly suitable for:

  • Large plastic components requiring relatively thick walls.
  • Industrial equipment covers with integrated supporting features.
  • Rigid panels where lower part density is beneficial.
  • Components requiring stiffness without completely solid sections.

Traditional injection molding is often more appropriate for thin-walled components, small functional features, and parts requiring demanding dimensional tolerances.

However, mechanical strength depends on resin selection, wall thickness, loading conditions, and internal structure. Structural foam does not automatically provide greater strength than solid plastic.

3. Differences in Tooling and Production Costs

Low-pressure structural foam molding can reduce cavity pressure compared with conventional high-pressure injection molding.

For suitable large components, this may allow different tooling construction and potentially lower mold investment.

Cost FactorStructural Foam MoldingTraditional Injection Molding
Mold ConstructionLower-pressure tooling may be possibleDesigned for specified injection pressures
Material ConsumptionReduced through cellular structureSolid material in molded sections
Equipment RequirementsSpecialized foam processing or blowing agentsConventional injection molding equipment
Cooling TimeInfluenced by thick walls and foamingInfluenced by geometry and wall thickness
Secondary FinishingMay require painting or surface treatmentOften fewer cosmetic finishing requirements

WIT Mold manufactures conventional plastic molds alongside structural foam tooling, allowing mold construction to be matched to the intended product.

For purchasing decisions, total manufacturing cost should include tooling, resin consumption, cycle time, finishing, and production volume.

4. Surface Finish and Dimensional Accuracy

Surface appearance is one of the most important differences between these processes.

Structural foam molded parts may develop swirl marks or streaks because of gas expansion during molding. These characteristics may be acceptable for industrial components but unsuitable for products requiring high-gloss cosmetic surfaces.

Traditional injection molding often provides greater flexibility for achieving smooth, detailed surfaces directly from the mold.

Important considerations include:

  • Cosmetic Requirements: Visible structural foam surfaces may require painting or finishing.
  • Dimensional Tolerances: Conventional injection molding may be preferable for demanding precision features.
  • Wall Thickness: Structural foam generally requires sufficient thickness for cellular development.
  • Part Geometry: Fine details and intricate thin sections may be better suited to conventional tooling.

WIT Mold supports structural foam molded components such as plastic covers, panels, handles, and equipment enclosures.

5. Which Process Is Better for Large Plastic Components?

The following examples illustrate how manufacturing requirements influence process selection.

Product ApplicationRecommended ProcessMain Reason
Industrial Machine HousingStructural foam moldingLarge size and structural rigidity
Plastic PalletStructural foam molding, where load requirements permitThick sections and material efficiency
Large Equipment PanelStructural foam or conventional moldingDepends on appearance and dimensional requirements
Thin-Walled Electronic HousingTraditional injection moldingThin sections and detailed features
Precision Plastic ConnectorTraditional injection moldingCritical dimensions and fine geometry
Large Structural CoverStructural foam moldingIntegrated supporting features

Structural foam molding is particularly attractive for large, thick-walled components where stiffness and material efficiency matter more than a high-gloss finish.

Traditional injection molding remains a strong choice for detailed components with tighter tolerances or demanding appearance requirements.

6. What to Confirm Before Choosing a Molding Process

Before deciding between structural foam and conventional injection molding, prepare the technical requirements that affect manufacturing feasibility.

  • Part Dimensions: Confirm overall size, wall thickness, and structural features.
  • Material Requirements: Specify the resin grade and mechanical properties.
  • Surface Finish: Define cosmetic requirements and acceptable secondary finishing.
  • Mechanical Loads: Identify stiffness, impact, and load-bearing requirements.
  • Dimensional Tolerances: Highlight critical assembly features.
  • Production Volume: Provide estimated annual demand for tooling cost evaluation.

WIT Mold develops custom tooling according to product drawings, material requirements, and production specifications.

Frequently Asked Questions

Is structural foam molding cheaper than traditional injection molding?

It can be more economical for large, thick-walled components because low-pressure processing may reduce tooling requirements and cellular structures can reduce resin consumption. Actual costs depend on mold complexity, production volume, cycle time, and finishing requirements.

Is structural foam molding stronger than conventional injection molding?

Not necessarily. Structural foam can offer useful stiffness relative to its weight, but solid injection molded parts may provide higher strength for the same geometry and material. Mechanical performance must be evaluated for each design.

Can structural foam molding produce smooth surfaces?

Structural foam parts may have visible swirl marks or surface irregularities. Painting, filling, or other secondary finishing operations may be required for demanding cosmetic applications.

Custom Structural Foam and Injection Mold Manufacturing With WIT Mold

WIT Mold manufactures custom structural foam molds and conventional injection molds for industrial equipment, commercial products, and large plastic components.

Our services include mold engineering, tooling manufacturing, sample verification, and production support based on customer requirements.

Contact WIT Mold to submit your CAD drawings, material specifications, and production requirements for a custom structural foam mold quotation.

Plastic Injection Mold Types Explained for Product Development

Choosing the right plastic injection mold type is essential during product development. Mold structure affects tooling costs, product quality, production efficiency, and manufacturing flexibility. Different plastic components require different tooling solutions depending on their geometry, material, and production volume.

WIT Mold has manufactured custom plastic molds since 2011, providing tooling solutions for automotive, electronics, household appliances, and industrial applications. Understanding the main injection mold types helps product developers select suitable tooling before investing in production.

1. Single-Cavity Injection Molds

A single-cavity mold produces one plastic component per injection cycle. It is commonly used for larger components, lower production volumes, and projects where individual part control is important.

Key advantages:

  • Lower initial tooling investment compared with many equivalent multi-cavity designs.
  • Simpler mold structures and maintenance requirements.
  • Suitable for product development and lower-volume manufacturing.

However, single-cavity molds have limited output per cycle, making them less economical for some high-volume applications.

2. Multi-Cavity Injection Molds

Multi-cavity molds produce several identical components during one injection cycle. They are commonly selected for mass production of small and medium-sized plastic products.

Key advantages:

  • Higher production output per molding cycle.
  • Potentially lower unit costs at sufficient production volumes.
  • Efficient use of injection molding machine capacity.

Multi-cavity tooling requires careful runner balancing, cooling design, and cavity consistency.

WIT Mold provides high cavitation molds for projects requiring increased production output.

3. Two-Shot Injection Molds

Two-shot molds, also called 2K injection molds, combine two materials or colors into a single finished component through sequential injection processes.

Typical applications include soft-touch handles, multi-color buttons, automotive controls, and plastic components with integrated grip or sealing features.

Key advantages:

  • Combines different material properties in one component.
  • Reduces the need for some secondary assembly operations.
  • Supports multi-color and rigid-soft product designs.

Two-shot tooling requires compatible materials and suitable molding equipment. WIT Mold manufactures two-shot injection molds for customized multi-material components.

4. Insert Injection Molds

Insert molding places a preformed component, often metal, inside the mold before plastic is injected around it.

This process is commonly used for electrical connectors, threaded inserts, structural components, and products requiring integrated metal-plastic construction.

Key advantages:

  • Integrates multiple materials into one molded component.
  • Can reduce post-molding assembly operations.
  • Supports reinforced or functional connection features.

Accurate insert positioning and appropriate molding conditions are essential to prevent defects and maintain component quality.

5. Unscrewing Injection Molds

Unscrewing molds are designed for plastic parts containing internal or external threads that cannot be released through straightforward mold opening.

A mechanical or powered unscrewing mechanism releases threaded features before part ejection.

Common applications include threaded caps, closures, fittings, and industrial plastic connectors.

These molds can produce complex threaded features directly, although their moving mechanisms generally increase tooling complexity and maintenance requirements.

6. High-Precision Injection Molds

High-precision molds are designed for components requiring demanding dimensional accuracy, detailed geometries, or consistent part fit.

They are frequently used for electronic components, precision mechanical parts, and products with strict assembly requirements.

Key considerations:

  • Precision machining and mold assembly.
  • Controlled material shrinkage and cooling.
  • Dimensional inspection and mold trial verification.
  • Suitable mold steel and tooling construction.

Unlike cavity count or molding method, precision describes the accuracy requirements of the tool and can apply to several mold types.

Comparison of Plastic Injection Mold Types

Mold TypeBest Suited ForMain Consideration
Single-Cavity MoldLower-volume or larger componentsLower output per cycle
Multi-Cavity MoldHigh-volume identical partsHigher tooling complexity
Two-Shot MoldMulti-material or multi-color componentsMaterial and equipment compatibility
Insert MoldMetal-plastic integrated componentsInsert positioning accuracy
Unscrewing MoldThreaded plastic componentsMechanical complexity
High-Precision MoldTight-tolerance componentsMachining and inspection requirements

How to Choose the Right Injection Mold Type

The most suitable mold depends on the product’s design and manufacturing requirements.

  • Production Volume: Higher quantities may justify multi-cavity tooling to reduce unit costs.
  • Part Geometry: Threaded features, undercuts, and complex structures may require specialized mechanisms.
  • Material Requirements: Multi-material products may benefit from two-shot or insert molding.
  • Dimensional Tolerances: Precision components require appropriate mold construction and inspection.
  • Tooling Budget: Initial investment should be balanced against expected production quantities and long-term costs.

For example, a simple plastic housing produced in limited quantities may only require conventional single-cavity tooling. A high-volume packaging component may benefit from a multi-cavity mold, while a soft-touch automotive button may require two-shot molding.

Frequently Asked Questions

Which injection mold type is best for mass production?

Multi-cavity molds are often suitable for high-volume production because they manufacture multiple identical parts per cycle. However, the optimal cavity count depends on part size, material, and machine capacity.

What is the difference between two-shot molding and insert molding?

Two-shot molding combines two injected materials or colors, while insert molding encapsulates a preformed component, such as a metal insert, within molded plastic.

Are complex injection molds more expensive?

Generally, molds requiring additional cavities, moving mechanisms, or specialized processing involve higher initial tooling costs. The final cost depends on mold size, complexity, materials, and production requirements.

Custom Plastic Mold Manufacturing With WIT Mold

WIT Mold provides custom injection mold design and manufacturing for different product structures and production requirements. Our capabilities include conventional molds, multi-cavity tooling, two-shot molds, insert molding tools, and specialized injection molds.

We develop mold structures based on customer drawings, plastic materials, expected production quantities, and dimensional requirements.

Contact WIT Mold to submit your product drawings and request a custom injection mold quotation.

Questions to Ask Before Working With a Plastic Mold Factory

Working with a plastic mold factory requires clear technical requirements and purchasing agreements. Before placing an order, OEM companies and procurement managers should confirm the factory’s capabilities, tooling specifications, inspection procedures, and delivery arrangements.

WIT Mold has manufactured custom plastic molds since 2011, serving international customers across automotive, electronics, household appliances, and other industries. The following questions can help avoid misunderstandings and ensure smoother tooling projects.

1. Can You Manufacture Molds According to Our Drawings?

Before discussing prices, confirm whether the factory can manufacture tooling that meets your product design and production requirements.

Ask about:

  • CAD Compatibility: Can the factory work with STEP, IGES, and detailed 2D engineering drawings?
  • Design Review: Will engineers evaluate wall thickness, draft angles, gate locations, and possible molding defects?
  • Tolerance Requirements: Can the specified critical dimensions be achieved and verified?
  • Mold Complexity: Does the factory have experience with sliders, lifters, threaded components, or multi-cavity tooling?

WIT Mold manufactures conventional injection molds and high precision molds for projects with different structural and dimensional requirements.

2. What Specifications Are Included in the Mold Quotation?

A mold quotation should clearly identify what the customer is purchasing. Different tooling specifications can lead to significant price differences.

QuestionInformation to Confirm
What mold steel will be used?Core, cavity, and mold base materials
How many cavities are included?Single-cavity or multi-cavity configuration
What runner system is proposed?Cold runner or hot runner
What is the expected mold life?Agreed production cycle target
Are mold trials included?Number of trials and sample submissions
Are spare components included?Replacement parts and additional charges

Request written confirmation of important specifications before approving the quotation.

3. How Do You Control Mold Manufacturing Quality?

Quality inspection should take place throughout the manufacturing process, not only before shipment.

Important questions include:

  • How are mold steel and purchased components inspected?
  • How are critical dimensions checked during machining?
  • What procedures are used to verify mold assembly?
  • Will dimensional inspection reports be provided?
  • How are defects identified and corrected during mold trials?

WIT Mold follows an integrated quality control process involving inspection procedures across mold design, machining, assembly, and final verification.

4. What Happens If the First Mold Trial Fails?

Initial mold trials may reveal dimensional deviations, filling defects, warpage, or ejection problems. These issues should be addressed before final mold acceptance.

Clarify whether the factory will:

  • Identify the cause of defects and recommend corrective actions.
  • Provide updated samples after tooling adjustments.
  • Submit inspection results for critical dimensions.
  • Explain how modifications affect project schedules.
  • Distinguish manufacturing corrections from customer-requested design changes.

WIT Mold’s tooling workflow includes mold trials and sample confirmation before proceeding to the next production stage.

5. What Are the Lead Time and Payment Terms?

A reliable mold factory should provide a project-specific manufacturing schedule rather than an unsupported delivery promise.

Before ordering, confirm:

  • Tooling Lead Time: Estimated time for design, machining, assembly, and mold trials.
  • Payment Schedule: Deposit requirements and remaining payment milestones.
  • Modification Costs: Charges associated with customer-requested engineering changes.
  • Shipping Terms: Packaging, transportation responsibilities, and agreed Incoterms.

All commercial conditions should be included in the purchasing agreement.

6. Who Owns the Mold After Manufacturing?

Mold ownership is particularly important for OEM companies planning long-term production.

Confirm who owns the completed tooling, whether technical documentation will be supplied, and whether the mold can be transferred to another manufacturing facility.

Maintenance responsibilities, replacement components, and future engineering modifications should also be discussed before placing an order.

Plastic Mold Factory RFQ Checklist

The following information helps manufacturers prepare accurate quotations.

Required InformationDetails
Product Drawings3D CAD models and 2D drawings
Plastic MaterialResin type and specified grade
Production QuantityEstimated annual demand
Critical DimensionsTolerances and assembly requirements
Surface FinishPolishing, texture, and appearance
Tooling RequirementsExpected mold life and cavity preferences
Delivery RequirementsTarget schedule and shipping destination

Complete project information reduces repeated clarification and helps establish realistic tooling proposals.

Frequently Asked Questions

What should I prepare before contacting a plastic mold factory?

Prepare CAD files, technical drawings, plastic material specifications, expected production quantities, and critical dimensional requirements. Include your target delivery schedule if available.

Can mold specifications be changed after an order is placed?

Yes, but changes may affect tooling costs and lead times. Engineering modifications should be reviewed and approved before implementation.

Should I approve mold samples before shipment?

Yes. Sample approval helps confirm that molded parts meet agreed dimensional, functional, and appearance requirements before final tooling acceptance.

Discuss Your Custom Plastic Mold Project With WIT Mold

WIT Mold provides custom injection mold design and manufacturing services for international OEM customers. Our capabilities cover conventional plastic molds, precision tooling, engineering coordination, and mold trial verification.

We manufacture tooling according to customer drawings, material requirements, and production specifications, with quality control integrated throughout the manufacturing process.

Contact WIT Mold to submit your CAD files, confirm tooling specifications, and request a quotation for your custom plastic mold project.